
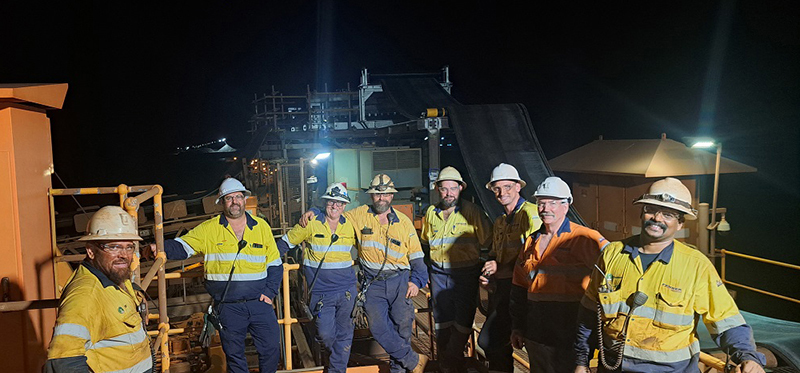
In 2025 Fenner successfully completed the replacement of a major wharf conveyor belt in the Pilbara. Traditionally, to conform to the strict safety and operational requirements around this system, replacements required six splices with smaller reels, or the deployment of a jack-up barge for full-length reels, a costly and risky marine operation.
With help from Belle Banne’s team of belt handling specialists, Fenner Conveyors devised an alternative solution involving an adjacent conveyor and a Belle Banne pony drive to feed the belt from land.
This innovative method significantly reduced manual handling and improved safety by eliminating the need for marine lifting and reducing the splice count from six to four.
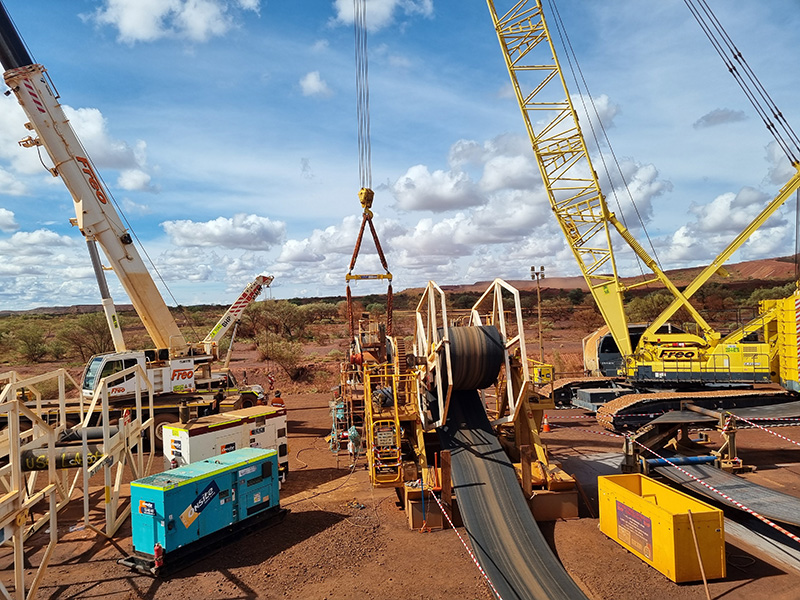
In 2024, the Belle Banne Belt Handling team facilitated the installation of a complex conveyor system at a Jimblebar mine, including a 333-meter-long conveyor belt flaking station. This was the longest single structure ever supplied by Belle Banne Belt Handling and required a custom methodology and meticulous attention during the seven-day installation.
In addition to the installation, Belle Banne engineers trained site personnel to operate the belt handling equipment safely and effectively. Several components, such as the Hydraulic Pony Drive, were new to site personnel, and the training ensured long-term system effectiveness.
The successful completion of the Jimblebar project reinforced Belle Banne Belt Handling as the leading equipment for specialised, highly engineered belt installation and change-out projects.

In 2023, a client operating an iron ore port facility contacted Fenner regarding their outload belts, which required replacement every 12 weeks due to the highly abrasive environment. They were seeking a 20% improvement in belt wear performance.
Fenner delivered a 50% improvement, extending the shutdown cycle from 12 to 24 weeks. This resulted in significant cost savings, improved efficiency, and reduced injury risk.
This success was achieved through the custom design and manufacture of a high-abrasion-resistant rubber compound known as UltraTuff. Fenner conducted comprehensive QA testing and provided an embedded engineering resource to manage the product’s lifecycle and ensure optimal performance.
Learn more about UltraTuff and read the full case study here.
Hancock Iron Ore approached CPS with a tight deadline for a pulley system, including a custom THDD bearing housing - typically a lead time challenge due to outsourced fabrication.
As part of CPS’s commitment to agile, reliable supply for Australian mining operations, our team brought the manufacturing in-house, prioritised the project, and delivered it on time in just 6.5 weeks. This also resulted in significant cost savings by avoiding external supply.
The bearing housings were finished in pink, supporting Hancock Iron Ore’s ongoing Breast Cancer Awareness initiatives. This continued Fenner Conveyors’ proud tradition of participating in awareness projects, including a pink belt winder manufactured in 2024 and pink conveyor roller flingers to HIO sites.


Our iBelt technology suite offers digital solutions for a wide range of belt monitoring applications, helping clients move away from traditional paper-based recordkeeping. It enables better tracking of belt wear, replacement schedules, and more.
Earlier this year, our team undertook an ambitious project to deploy mobile BeltGauge monitoring units from the iBelt suite across five different belts, some of which travelled distances up to 29 km.
The site’s previous thickness testing methods provided only 1D cross-sectional measurements, insufficient for detecting localised damage or wear.
With their new monitoring system, the operation will be able to detect belt damage before it escalates, optimise their maintenance schedules and prevent costly operational disruptions. Ongoing data collection will be supported by Fenner’s service teams as part of our commitment to aftermarket support.
As Fenner continues to innovate in intelligent conveyor technologies, projects like this show our commitment to delivering smarter, more efficient solutions to Australian mining.


